| Primary application |
Suitable for applications where cards are replaced frequently and exposure to magnetic fields is limited. |
Suitable for cards expected to remain in service longer or operate near stronger magnetic fields. |
Choose a machine that supports the required stripe material and the downstream encoding process. Coercivity must be confirmed from the stripe supplier or card specification. |
| Coercivity requirement |
Nominal target: 300 Oe. |
Nominal target: 2,750 Oe. |
Use a coercivity-capable magnetic test system for incoming inspection. Do not determine coercivity from stripe color alone. |
| Common stripe color |
Often brown, but color is not a reliable technical identification method. |
Often black, but color is not a reliable technical identification method. |
Configure the machine according to measured material properties, not visual appearance. |
| Standard card format |
For an ISO/IEC 7810 ID-1 card, the nominal finished card size is 85.60 mm × 53.98 mm, with a nominal thickness of 0.76 mm. |
Verify that the card conveyor, guide rails, vacuum plate, and clamping system support the actual card dimensions and thickness tolerance. |
| Magnetic stripe width |
A conventional full-width magnetic stripe is commonly specified at approximately 12.7 mm, subject to the applicable card and stripe standard. |
Use adjustable strip guides and a controlled placement system. Confirm the actual stripe width and location against the production drawing before ordering tooling. |
| Placement accuracy |
Recommended planning target: ±0.25 mm or better for repeatable visual alignment. |
Recommended planning target: ±0.25 mm or better for repeatable visual alignment. |
Ask for measured placement capability using the intended card substrate, adhesive, stripe roll, and operating speed. The final tolerance must follow the product drawing. |
| Strip application method |
Pressure-sensitive adhesive or heat-assisted bonding may be used, depending on the stripe construction. |
Pressure-sensitive adhesive or heat-assisted bonding may be used, depending on the stripe construction. |
Select unwind tension control, nip rollers, heated rollers, or compression tooling only after confirming the stripe adhesive and substrate compatibility. |
| Material compatibility |
Commonly applied to PVC, PET, or composite card constructions when the adhesive system is compatible. |
Commonly applied to PVC, PET, or composite card constructions when the adhesive system is compatible. |
Request compatibility trials for the exact card material. Check adhesion, edge lift, bubbles, wrinkles, and surface damage after bonding. |
| Recommended line-speed range |
A planning range of 20–60 cards per minute is typical for semi-automatic or compact automatic mounting lines, but actual output depends on card size, strip length, inspection, and handling. |
Require a site trial at the desired speed. Compare good-card output, not only the machine's no-load cycle rate. |
| Unwind and tension control |
Stable, low-tension unwinding helps prevent stretching, curling, and edge deformation. |
Stable, low-tension unwinding helps prevent stretching, curling, and edge deformation. |
Look for a controlled unwind, dancer arm or equivalent tension feedback, adjustable braking, and a strip-break or end-of-roll sensor. |
| Bonding pressure |
Pressure must be sufficient for full adhesive contact without imprinting the stripe surface. |
Pressure must be sufficient for full adhesive contact without imprinting the stripe surface. |
Prefer adjustable nip pressure and replaceable rollers. Validate pressure settings through peel, visual, and functional tests. |
| Position detection |
Optical or registration-mark detection can control leading-edge and lateral placement. |
Optical or registration-mark detection can control leading-edge and lateral placement. |
Specify sensor response, guide adjustment range, automatic correction, and rejection of cards with missing or misaligned stripes. |
| Magnetic performance check |
Verify the 300 Oe stripe's signal level, recorded data quality, and readability after mounting. |
Verify the 2,750 Oe stripe's signal level, recorded data quality, and readability after mounting. |
Use a calibrated magnetic-stripe analyzer or encoder/reader test station. Test before and after mounting to identify process-related signal loss. |
| Typical defect controls |
Monitor scratches, incomplete transfer, bubbles, wrinkles, edge lift, and low signal caused by excessive pressure or heat. |
Monitor scratches, incomplete transfer, bubbles, wrinkles, edge lift, and low signal caused by excessive pressure or heat. |
Specify automatic detection for missing strips, double feeds, skew, splice joints, and out-of-position application where production volume justifies automation. |
| Changeover requirements |
Adjustments may be needed for stripe width, roll core, card thickness, and adhesive construction. |
Adjustments may be needed for stripe width, roll core, card thickness, and adhesive construction. |
Prioritize tool-free guides, recipe storage, digital counters, quick-clean access, and clearly marked setup references. |
| Best purchase choice |
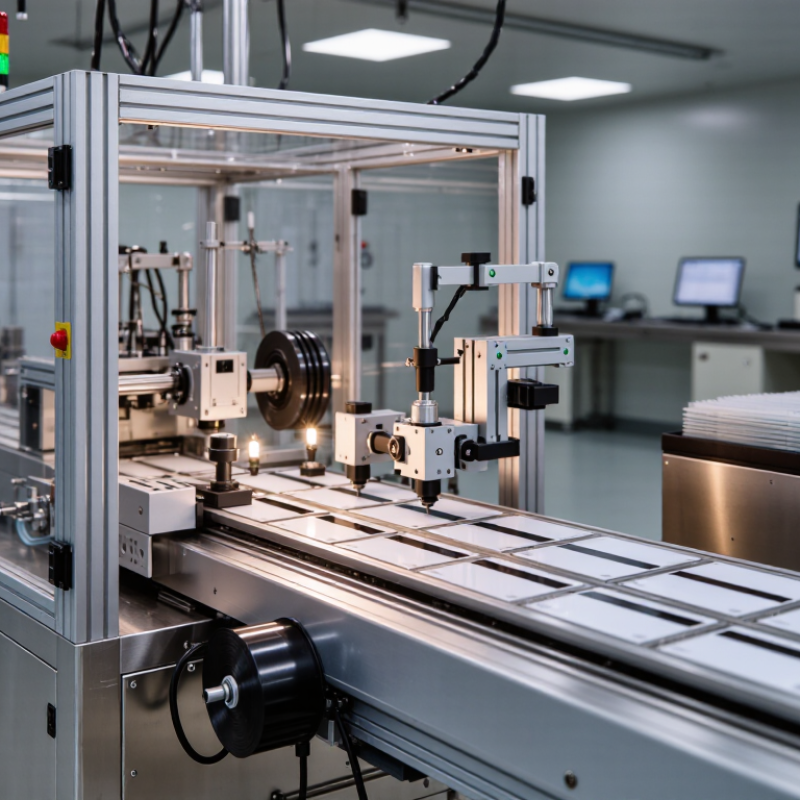
Choose a low-tension, accurate mounting system with gentle handling and reliable post-application magnetic testing. |
Choose a robust mounting system with accurate registration, controlled pressure, and verified compatibility with high-coercivity stripe media. |
The best machine is the one that passes a production trial using the exact LoCo or HiCo stripe, card body, adhesive construction, target speed, and inspection criteria. |
 Wentong Machinery